Sheet metal prototyping is not a smaller version of production. It is a different job with a different goal: production proves a process, while a prototype proves a design. The questions a sample round should answer are narrow and expensive to guess wrong — does the enclosure assemble, do the holes line up, does the finish read right, and what will the batch actually cost per piece. Get those four answered on one sample, and the batch becomes execution. Guess them, and you learn the same lessons on five hundred cabinets.
SanJun Hardware started more than fifteen years ago on exactly this route: sheet metal fabrication, sketch-to-sample work, and batch production. Today a 5,000 m² facility in Guangdong, China runs the same path for OEM customers — one sample unit, a pilot batch, then production, with the sample charge credited back when the order follows.
A prototype buys information, and the information has a hierarchy.
Fit comes first. A drawing can show every part dimensionally correct and still fail at assembly: a rivet nut too close to a bend line, a hinge hole that lands on a weld seam, a door that binds when the internal rail is loaded. One physical set closes those questions in a day; a spreadsheet argues about them for a week.
Function comes second. Vent positions get checked against real board layouts, gasket channels against actual door flatness, cable routes against the harness you intend to install. These are the failures that survive a good-looking drawing.
Cost comes third, and it is the one buyers skip. A design that assembles with two people in thirty minutes and one that needs a welder, a grinder, and an afternoon produce the same cabinet and different unit prices. The sample round is when you find out which one you drew.
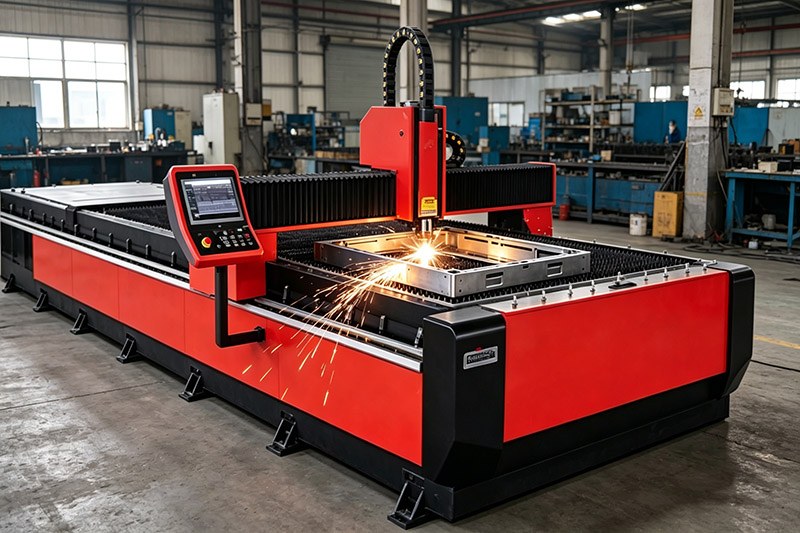
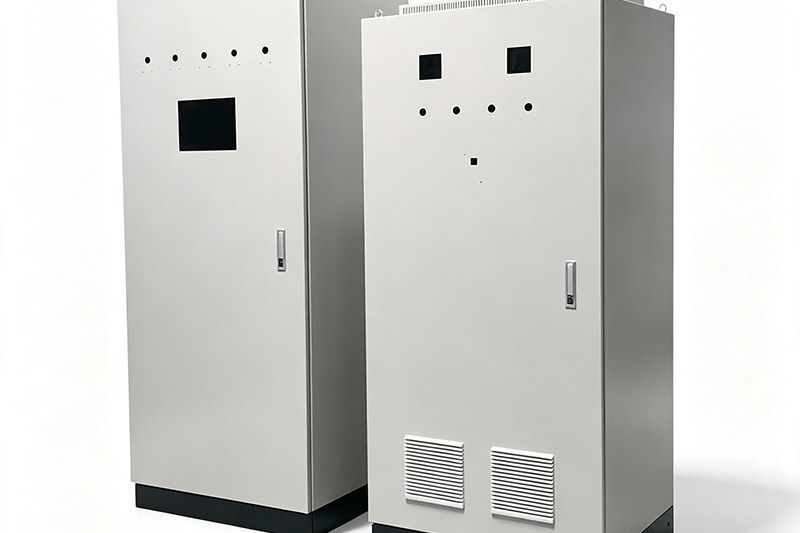
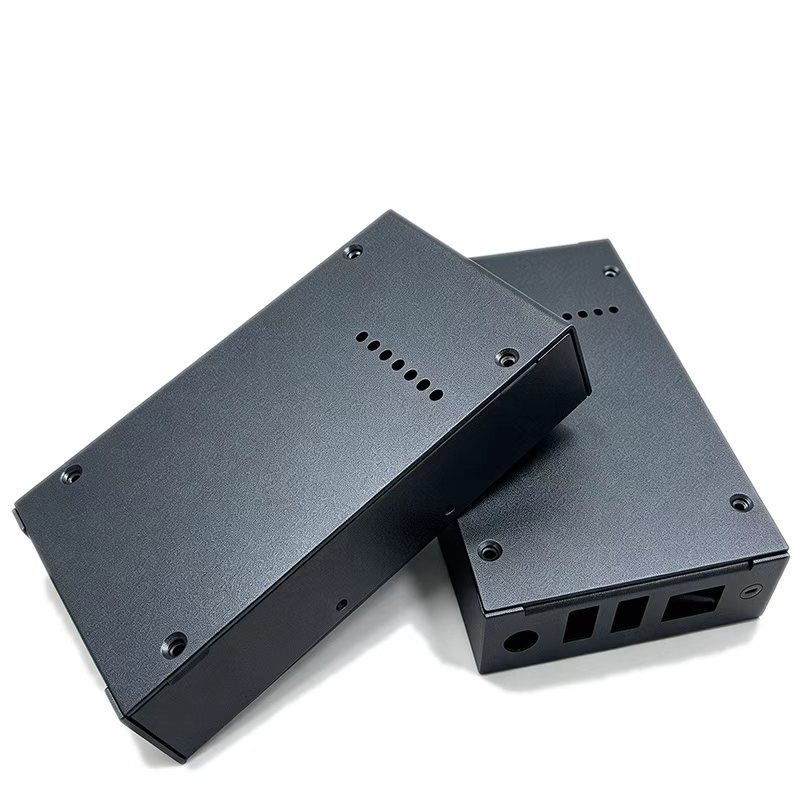
The first sheet metal prototyping sample usually needs no dedicated tooling. Laser cutting and CNC punching form the blanks, a press brake with standard tooling forms the bends, and welding, riveting, and finishing complete the unit. That is why a one-piece MOQ is practical for enclosures: the factory changes a nesting file, not a die.
Where a design genuinely needs stamping, fixtures, or a custom die, that decision moves to the DFM review, before metal is cut. Our engineers review drawings, sketches, or 3D models in a free CAD design review and flag the features that would create tooling cost — then suggest the formed-or-riveted alternative where it holds. If your starting point is a sketch or a physical sample rather than a CAD file, our guide to converting sketches and samples into production-ready CAD covers that front end.
A sample that "looks right" proves nothing. The acceptance round should run against the same checks the batch will face.
– Key dimensions on a coordinate measuring machine and a projector, with tolerance callouts from the drawing — not a tape measure.
– Assembly fit against your real modules. Bring the board, the rail, the display. A housing tested against air passes and fails on site.
– Finish against a signed standard: color, gloss, texture, and the adhesion result from a cross-hatch test on the same batch of coated parts.
– Functional tests where the design claims them: water spray for a sealed door, salt spray coupons for a coating system, hinge cycles for a service door.
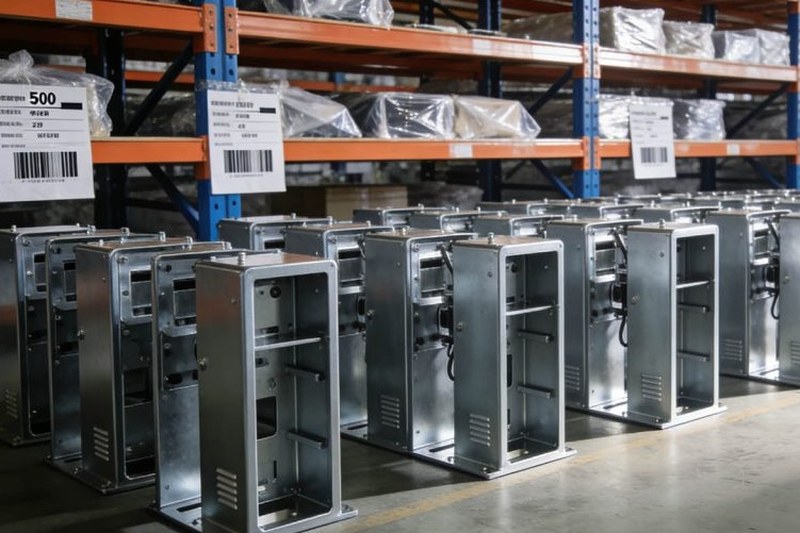
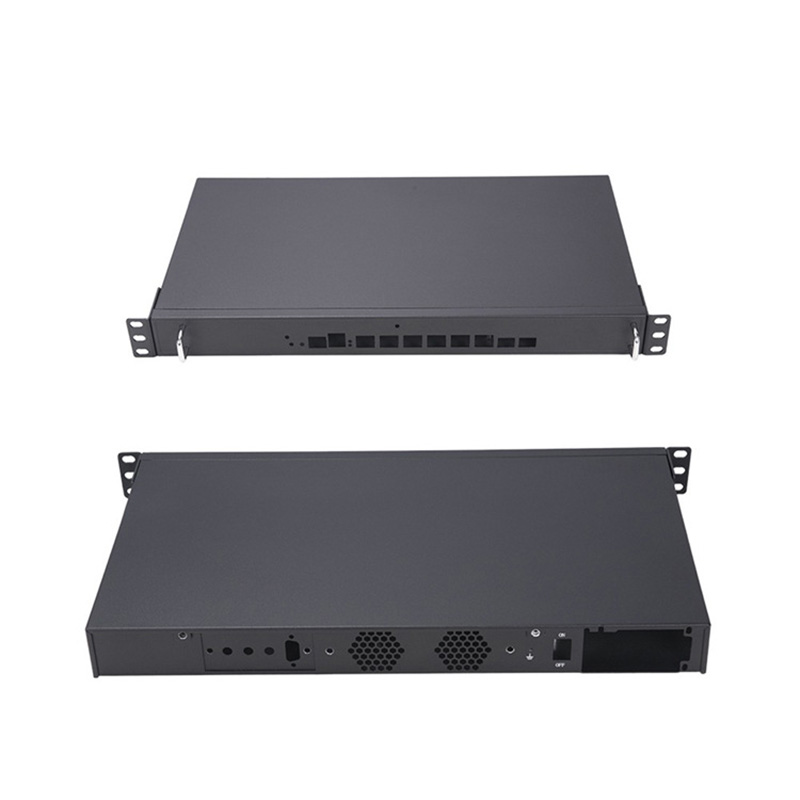
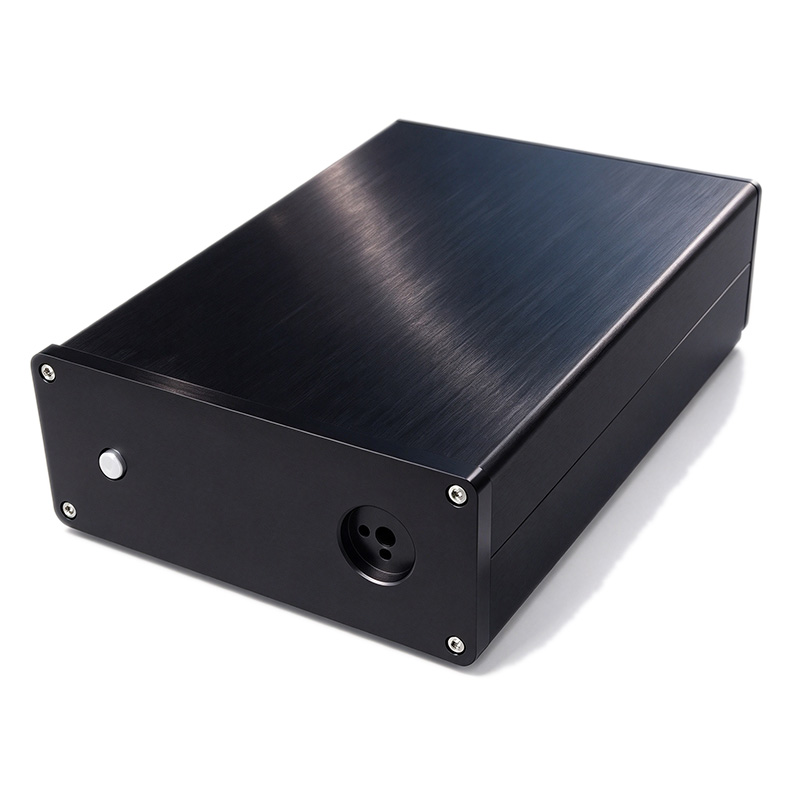
Every process step in our shop carries a QC checkpoint, so the sample report reflects the inspection plan your batch will run under. On a precision server chassis, for example, hole-position accuracy across the side panels is exactly the thing a single sample exposes and a rendering never will.
The honest answer on minimum order quantity is: it depends on the structure. Our working range starts from a single sample, moves to pilot batches around 100 pieces, and goes below that when the design needs no dedicated tooling and the material lot is already open. What actually drives a floor on quantity is setup: program time on the laser and brake, weld fixture adjustment, coating line changeover. A part that reuses existing programs and powder colors can run in twenties. A part with a custom die cannot sensibly run under hundreds.
The commercial logic pairs with this: sample and pilot quantities are priced as engineering work, production quantities as manufacturing work. The sample fee credited against the volume order means the prototype round is not a sunk cost once you proceed — it is the first units of your program.
The sheet metal prototyping round ends when the design stops changing. A pilot batch then moves the question from "does the design work" to "does the process repeat." Between the approved sample and the first production order, three things get locked: the drawing revision under change control, the inspection plan with its QC checkpoints, and the packaging method for your shipping lane.
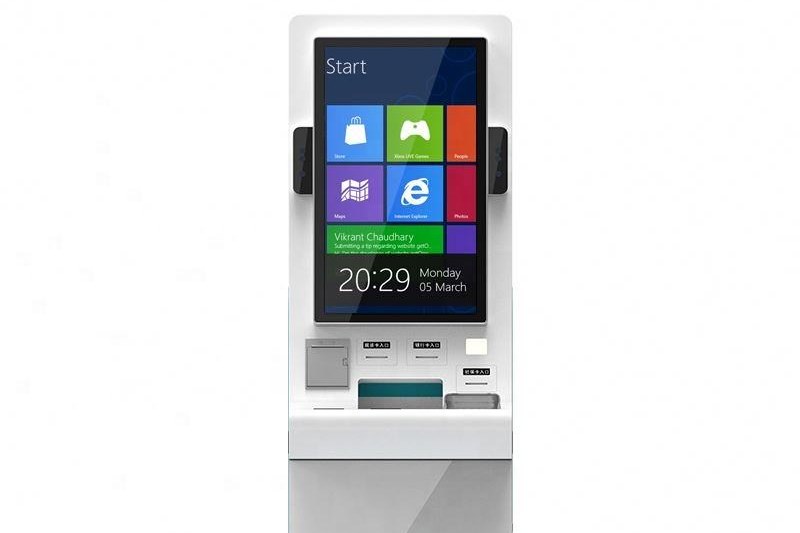
Drawing changes after the sample are normal, and they are managed, not absorbed: each revision goes through review, cost impact, and process adjustment before it enters production. A provincial tertiary hospital program we ran — 200 registration and payment terminal enclosures — moved through design, prototypes, batch production, and installation support as one chain, with the sample round fixing the final panel layout before the first production door was cut.
Standard structures run 7–15 working days; custom housings with new detailing take 20–30 or longer. Quotes come back within 24 hours of a drawing or requirement list, and the CAD review happens before you commit anything. Shipments leave under FOB, CIF, or DDP terms in plywood crates with foam, VCI film, and desiccant, with a 12–24 month warranty on fabrication quality.
A realistic first order is a sample plus a pilot batch plus a production forecast — three numbers, one conversation. That shape lets the factory reserve capacity and lets you stop after the pilot if the market answer is no.
Sheet metal prototyping works when each round is given one job: the sample settles design risk, the pilot settles process risk, the order settles capacity. A fabrication partner that can run all three from the same drawings, the same machines, and the same inspection plan removes the handover losses that make overseas programs slow. The one-piece start and the credited sample fee exist to make that first round cheap enough to say yes to.
اتصل بمتجر سانجون للأدوات المنزلية to send a drawing, book the free CAD review, and start with a single sample before you commit to a batch.
A: Simple enclosures can come back inside the standard-part window of 7–15 working days; designs with new forming, welding fixtures, or coating matches typically take 20–30. The CAD review flags which category your part falls into before the clock starts.
A: The sample fee is charged as engineering work and credited against the volume order when you proceed. If the program stops after the pilot, the fee stays with the factory — which is why the pilot quantity is sized to answer the question, not to stock a warehouse.
A: Yes, through change control. Each revision is reviewed for cost and process impact before production adopts it, and the inspection plan updates with it. Changes made quietly against an old revision are the classic cause of a batch that no longer matches the approved sample.
A: That is a process problem, not a design problem, and it is caught by QC checkpoints at each step rather than a final inspection alone. Ask for the sample’s measurement report and require production to run against the same checkpoint plan.

اترك تعليقات